
For industrial custom drive systems, peak performance is not by chance. It comes from careful maintenance. Precision shaft alignment and rotor balancing are key.
Misaligned shafts make motors work harder, using more electricity. This raises energy costs. Laser alignment tools help avoid this waste.
Vibration from imbalance harms bearings. It leads to uneven load distribution. This causes bearings to fail early, causing downtime.
Shaft deflections also damage seals. A problem like soft foot makes this worse. It can lead to lubrication loss or contamination, harming the system.
Being precise in these areas is a smart move. It protects assets, keeps people safe, and saves money. For leaders, it’s essential for long-term success.
Steps: base flatness/soft‑foot → rough align → thermal growth offsets → final laser alignment
Aligning precision is a journey through four key steps. Each step builds on the last, ensuring a stable system. Skipping any step can shorten the machine’s life.
The journey starts with the foundation. Technicians check for base flatness and fix soft-foot issues. Soft-foot happens when a machine foot doesn’t sit flat, causing strain.
To fix this, shims are placed under the foot that’s not flat. This ensures all four corners have even contact. A stable base is essential for all adjustments.
After the base is set, the rough alignment begins. This uses dial indicators or a laser in its basic form. The aim is to get the units roughly in place.
This step gets the shafts close enough for the next fine-tuning. It saves time in the final, precise phase.
The next step is about thermal growth. Heat from operation causes parts to expand. If not aligned for heat, the machine will be off when it’s hot.
Engineers use data to predict this growth. They then adjust the alignment before it gets hot. This is done to counteract the expected expansion.
Handling thermal growth is key for experts. It keeps the alignment correct even when it’s hot. This is vital for high-temperature use.
The last step is laser alignment. Modern lasers offer accuracy down to microns. They measure misalignment in real-time.
Technicians adjust the machine feet based on the laser’s data. They aim for the tolerances set by coupling and bearing makers. This final check ensures the alignment meets design standards.
Following this order—foundation, rough, thermal, final—is critical. It ensures a reliable, precise drive system. This method avoids guesswork and guarantees a lasting alignment.
Coupling types and allowable misalignment
Choosing a coupling is not just about its torque. It’s also about how much it can handle in terms of parallel and angular offset. Each coupling has its own limits for misalignment. Going beyond these limits can cause early failure in machinery.
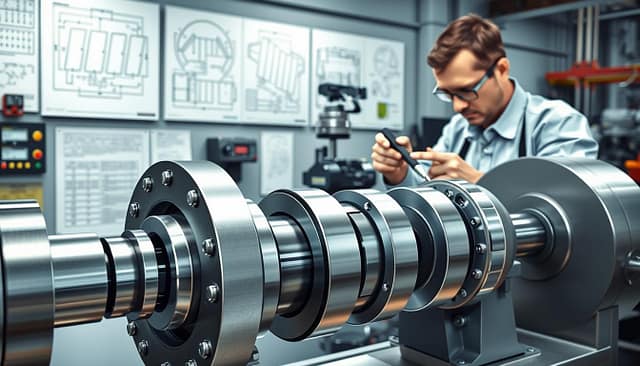
There are many types of couplings used in industry. Each has its own strengths and uses.
- Gear Couplings: Use internal and external teeth. They handle high torque and some misalignment but need oil.
- Grid Couplings: Have a spring-like element. They are flexible and absorb shocks well.
- Disc Couplings: Use flexible metal discs. They are stiff in torsion and control motion well.
- Elastomeric Couplings: Have rubber or polyurethane parts. They dampen vibrations and handle big misalignments.
- Metallic Membrane Couplings: Use thin, flexible metal. They are for high-speed, precise applications.
Misalignment is measured in three ways. Knowing these is key to setting alignment goals.
- Parallel Offset: The distance between shaft centerlines.
- Angular Misalignment: The angle of shaft divergence from a common axis.
- Axial Gap: The distance between coupling halves along the shaft axis.
Manufacturers set specific limits for each parameter based on the coupling’s design. The table below shows typical ranges for common couplings. Always check the manufacturer’s specs.
| Coupling Type | Parallel Offset (mils) | Angular Misalignment (degrees) | Axial Gap (inches) |
|---|---|---|---|
| Gear | 5 – 10 | 0.5 – 1.0 | 0.010 – 0.030 |
| Grid | 10 – 20 | 1.0 – 1.5 | 0.015 – 0.040 |
| Disc | 3 – 8 | 0.5 – 1.0 | Fixed |
| Elastomeric | 15 – 30 | 2.0 – 3.0 | 0.020 – 0.060 |
| Metallic Membrane | 2 – 5 | 0.25 – 0.5 | Fixed |
The reasons for these limits are complex. Design flexibility, material properties, and lubrication are key. Grid or elastomeric couplings can handle more misalignment because of their flexible parts. Disc or membrane couplings have tighter limits for better precision and stiffness.
Going beyond these limits can cause big problems. It puts too much stress on the coupling parts. This leads to wear, heat, and failure. The vibration then affects bearings and machine structures.
This vibration makes balancing the rotor harder. It can hide or make imbalance forces worse. So, keeping within the coupling limits is essential for good dynamic balancing.
Choosing the right coupling and sticking to its limits is critical. It ensures the alignment steps are precise and based on engineering. This protects the drive train from damage.
In‑place balancing workflow and acceptance criteria
The in-place balancing process starts by confirming that imbalance is the main cause of vibration. A detailed, systematic approach is key to getting consistent results and keeping machines in good shape. This method breaks down a complex task into simple, data-based steps.
First, a thorough vibration analysis is done. Technicians use portable analyzers to measure vibrations at key spots on bearings. This helps find where the imbalance is and if it needs correction in one or two planes.
For long rotors like fan shafts or multi-stage pump impellers, two-plane dynamic balancing is needed. Shorter rotors might only need correction in one plane. The method used depends on the machine’s shape and speed.
The core of the correction process involves trial weights. A known test weight is added to the rotor at a marked spot. The machine is then run at full speed, and new vibration readings are taken.
Special balancing software or vector calculations use this data. They figure out the exact weight and position needed to balance the rotor. The final weight is then put in place.
A final check run confirms the vibration has been reduced. This closed-loop process makes sure the correction is right and works.
There are clear standards for balancing work. ISO 1940 sets the quality standards, and ISO 10816 deals with vibration severity. Machines are grouped based on their design and function.
Each group has specific vibration limits, usually in inches per second (ips) or millimeters per second (mm/s). Meeting these limits is essential for reliable, long-term operation.
| Machine Class (Example) | ISO 10816 Vibration Severity Grade | Typical Allowable Velocity (ips) |
|---|---|---|
| Small Pumps, Motors (up to 15 kW) | B (Good) | 0.12 – 0.18 |
| Medium Fans, Turbines | B (Good) | 0.18 – 0.28 |
| Large Centrifugal Compressors | A (Excellent) | 0.08 – 0.12 |
Choosing the right balancing method is critical. The table below shows the main differences between single-plane and two-plane balancing. This choice affects the workflow and tools needed.
| Criteria | Single-Plane (Static) Balancing | Two-Plane (Dynamic) Balancing |
|---|---|---|
| Best For | Short, disk-like rotors (e.g., grinding wheels, impellers) | Long, shaft-like rotors (e.g., fans, turbines, extended motor shafts) |
| Correction Planes | One plane of correction is sufficient. | Requires weight correction in two separate planes along the rotor. |
| Common Tools | Static balancers, simple vibration meters. | Portable vibration analyzers with phase measurement, dynamic balancing software. |
| Outcome | Eliminates force imbalance; prevents bouncing. | Eliminates both force and moment imbalance; prevents rocking. |
Phase measurement is key in modern dynamic balancing. It shows not just how bad the vibration is, but where the heavy spot is on the rotor. This angle data is vital for placing weights correctly.
Acceptance means vibration levels meet ISO standards for the machine’s class. The “as-left” data is documented and compared to the “as-found” readings. A good balance job can cut vibration by 70% or more.
Combining balancing with laser alignment makes a strong reliability plan. Proper alignment ensures forces are right. Precise balancing removes shaking forces. Together, they help bearings and seals last longer.
Following this structured workflow makes balancing a science, not an art. It gives maintenance teams a clear path from finding faults to fixing them. This leads to smoother operation, less energy use, and longer machine life.
Documentation: as‑found/as‑left + photos in CMMS
Keeping detailed records is key to tracking asset history. For tasks like precision alignment, thorough records are essential. They help in strategic asset management and support informed decisions.
The “as-found” report captures the machine’s initial state. It includes the shaft’s alignment and soft foot measurements. These details are critical.
Vibration spectra before the service act as a benchmark. It’s important to note expected thermal growth. This initial data helps in diagnosing and planning corrective actions.
The “as-left” report shows the machine’s final state. It includes the laser alignment system’s final printout. Post-balancing, vibration levels and correction weights are documented.
Adding digital photos to CMMS work orders is a good practice. Photos should show setups, shim packs, and the final configuration. This visual proof ensures work quality.
A structured comparison of required data clarifies the documentation workflow. The table below outlines the core elements for each report type.
| Data Category | As-Found Report (Baseline) | As-Left Report (Final) |
|---|---|---|
| Alignment Data | Initial offset & angular misalignment | Final laser alignment printout; achieved tolerances |
| Foundation/Footing | Measured soft foot values at all mounts | Shim stack details & final foot load |
| Vibration | Baseline vibration spectra & overall levels | Residual vibration after balancing; ISO compliance |
| Operational Parameters | Assumed thermal growth offsets; operating temperature | Confirmed thermal compensation settings |
| Corrective Actions | N/A | Location & mass of all correction weights |
This disciplined approach offers strategic benefits. It supports internal audits and OEM warranty claims. It also enables trend analysis and knowledge transfer.
Consistent documentation is key to a solid maintenance strategy. It turns data into actionable intelligence. This ensures every job contributes to asset reliability and cost savings.
Learn more about audit-proof maintenance strategies here.
Common pitfalls and quick fixes checklist
Avoiding common errors ensures the longevity of your custom drives. This checklist highlights frequent missteps and their solutions.
Neglecting a soft-foot check is a primary error. Verify base flatness before any alignment. Use a feeler gauge or dial indicator. Correct soft-foot with proper shimming at the foot with the largest gap.
Failing to account for thermal growth leads to hot misalignment. Always input the correct thermal offset values into your laser alignment tool during the rough alignment phase. Use the machine’s operational temperature data.
Incorrect coupling gap setting causes premature wear. Follow the manufacturer’s specified gap. Measure the gap at multiple points around the coupling to ensure parallelism.
Using damaged or improper shims introduces instability. Only use clean, undamaged, full-contact shims. Stack no more than three shims under any foot. Tapered shims are not acceptable for precision work.
Improper use of laser alignment tools yields false readings. Ensure the sensors are securely mounted and the chain is taut. Always perform a sweep check to confirm the tool is calibrated. Document the “as-found” and “as-left” values.
Overlooking external forces like pipe strain can undo precise work. Check for connected piping stress after the final laser alignment. Loosen pipe hangers near the machine, re-tighten after alignment is complete.
Forgetting in-place balancing after alignment leaves vibration issues. Always perform a single-plane balance check on the assembled system. Follow the balancing workflow and adhere to the ISO 1940 acceptance criteria.
Effective precision maintenance is a cornerstone of predictive maintenance strategies. It provides the reliable data needed for accurate machine health monitoring. Addressing these pitfalls directly reduces downtime and extends asset life.


