
Manufacturing leaders face a big challenge on custom or mixed-model production lines. The mix of variable cycle times and complex product flows makes it hard to find true performance issues. A structured, data-driven approach is key for lasting gains.
Overall Equipment Effectiveness (OEE) is the core metric. It’s more than just a number; it’s a strategic framework for improvement. This roadmap turns OEE into a powerful tool for diagnosing issues.
The journey starts with a solid baseline. An effective OEE calculation must use a time-based method, not just a simple production count. This shows the real health of the line by accurately reflecting losses.
Good information leads to smart decisions. The IDA (Information, Decision, Action) method shows this. Before acting, manufacturers must correctly identify the line’s constraint. Its performance determines the total throughput.
This method, from precise measurement to targeted intervention, is at the heart of a successful structured approach to improve OEE. It matches a strict systematic workflow from concept to commissioning. This ensures every improvement is based on reliable data.
Loss tree: planned vs unplanned downtime, speed loss, defects/rework
Turning OEE data into action plans starts with a loss tree. This tree sorts out the real problems from the symptoms. A detailed loss tree turns a single percentage into a clear plan for improvement.
The Six Big Losses framework is the standard for categorizing losses. It breaks down inefficiencies into three main areas: Availability, Performance, and Quality.
https://www.youtube.com/watch?v=93l-d-lcWEQ
- Availability Losses stop production completely. This includes Breakdowns (equipment failure) and Setup and Adjustments (planned downtime for maintenance).
- Performance Losses happen when the line runs slower than it should. They are divided into Small Stops (minor interruptions) and Reduced Speed (running slower than the maximum rate).
- Quality Losses are for output that doesn’t meet standards. This includes Startup Defects (scrap during ramp-up) and Production Defects (scrap or rework during stable running).
First, we need to tell planned from unplanned downtime. Unplanned breakdowns are reactive and show reliability issues. Planned setups, though needed, can be reduced with SMED.
For lines with many steps, we need to analyze deeper. We look at the system’s constraint or bottleneck. This bottleneck analysis tags every loss event.
Teams must figure out if a stop was an Internal Stop or an External Stop. This tells us if the problem is at the bottleneck or elsewhere.
This helps us know where to focus for the biggest impact. Improving internal stops at the bottleneck has the most direct effect on throughput.
This method of loss analysis does more than just track data. It creates a clear plan for where to focus resources. By categorizing losses and looking at the bottleneck, managers can find the most costly inefficiencies. This turns generic OEE tracking into targeted bottleneck analysis and action.
Bottleneck mapping and buffer strategy
In any production system, the slowest operation limits the whole line’s output. This slow step is key to improving efficiency. Finding and managing this bottleneck is essential for better performance.
Finding the bottleneck starts with a detailed analysis. Look for the step where work piles up. This is often where material accumulates before a station.
Material buildup is a sign of a bottleneck. Mapping the flow of materials and information helps find it.
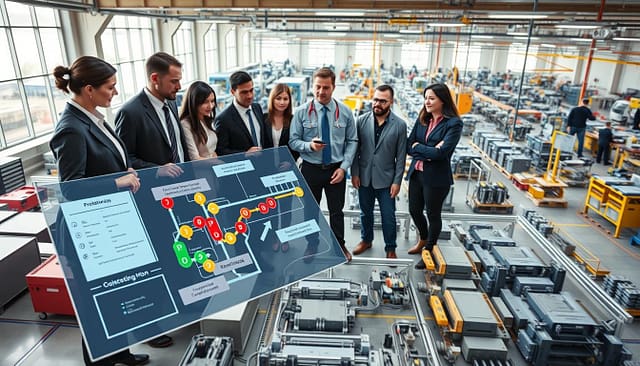
Measuring cycle time and throughput at each step helps map the process. This data shows where the bottleneck is without doubt. Once found, all efforts should focus on improving this station.
Improving other parts of the line won’t boost overall output. The bottleneck controls the pace. Using SMED here can make a big difference.
| Indicator | Description | Recommended Action |
|---|---|---|
| Persistent WIP Buildup | Inventory consistently stacks before a specific machine or operator. | Formally designate this station as the constraint and measure its exact cycle time. |
| Chronic Operator Waiting | Downstream stations are frequently idle, waiting for work from upstream. | Map the flow to confirm the bottleneck location and analyze its downtime reasons. |
| Longest Average Cycle Time | Data shows one station has a significantly longer processing time than others. | Focus on cycle time reduction techniques, including SMED for changeovers, at this location. |
| Highest Utilization Rate | A machine or resource is constantly in use, with no spare capacity. | Protect this resource with a buffer and prioritize its maintenance. |
After finding the bottleneck, the next step is to protect it. A buffer is placed before the bottleneck. It’s a small amount of inventory.
The buffer’s job is to keep the bottleneck stable. If upstream machines stop, the bottleneck can keep working. This ensures it’s always used to its fullest.
This buffer makes the bottleneck a reliable part of the line. The goal is to make it work as efficiently as possible. Improving the bottleneck’s uptime is the best way to increase efficiency.
Using SMED here can greatly increase line speed. Bottleneck mapping, buffer strategy, and SMED are key to unlocking its full power.
Quick wins: sensor health, auto‑cleans, standardized start‑ups
Starting with quick, easy actions is often the best way to improve OEE. These simple steps boost equipment reliability and process stability. They also help build team confidence and lay the groundwork for bigger projects.
Focus on areas the operations team can control. Early wins show the program’s value without needing a lot of money or outside help. This practical approach gets everyone on board and keeps the momentum going.
Three key areas offer quick, big wins:
- Keeping sensors in good shape for accurate data.
- Improving automated cleaning to save time.
- Setting up standard start-up and running procedures.
Sensor Health and Calibration is a key quick win. Bad or off sensors mean wrong data. Checking and fixing sensors is a simple way to get accurate data.
Teams can do simple maintenance tasks to fix this. They clean sensors, check their alignment, and make sure connections are good. Calibrating scales and temperature probes against a known standard also helps.
Automating Routine Cleans (Auto-Cleans) cuts down on planned downtime. Cleaning machines manually can take too long. Automating these tasks makes them faster and more consistent.
Setting up the right wash, rinse, and sanitize sequences in the machine’s PLC saves time. This quick fix doesn’t need new hardware but boosts equipment availability right away.
Standardized Start-ups and Running Procedures greatly reduce speed losses and minor stops. Different ways of setting up machines can cause problems. Creating clear, visual standard work for each product helps.
This standard work should be easy to find at the machine. It includes step-by-step start-up guides, the best settings, and approved changeover sequences. This way, everyone knows the right way to do things.
This standard work is not just about following rules. It turns tribal knowledge into a reliable process. It’s the foundation for further improvements.
These actions create a strong starting point. They make the process stable, improve team skills, and increase OEE. This sets the stage for tackling bigger challenges and improving even more.
Daily management: tier boards, andon alerts, short interval control
Daily management systems make OEE a key part of the shop floor culture. They keep improvements in availability, performance, and quality going. This approach helps teams focus on solving problems quickly and effectively.
The main challenge is keeping performance high without slipping back. Without daily routines, quick fixes become the usual solution. Daily management helps keep improvements and push for more.
Tiered communication boards are at the heart of this effort. They show important data like OEE, top losses, and key actions. This information moves up from team levels to management summaries.
This setup makes everyone see the big picture and share responsibility. Teams know their goals and how they did yesterday. Supervisors can quickly see where help is needed, promoting a culture of teamwork and problem-solving.
Andon alert systems highlight any issues right away. If a machine breaks down or quality drops, an alarm goes off. This stops the line from ignoring small problems that can cause big delays.
It lets operators call for help fast. This quick action is key to solving problems quickly. It’s the first step in finding the root cause of issues.
Short-interval control (SIC) meetings are key for managing proactively. They happen every two to four hours. Teams quickly review recent performance data.
This helps them catch problems early, like a slow speed or frequent stops. They can figure out why these issues happen and fix them right away.
Leadership support is key, shown through Gemba walks. When managers visit the shop floor, it shows they care. It also makes sure everyone knows the big goals and how to meet them.
Together, tier boards, Andon alerts, and SIC meetings create a strong system. They help teams work together to solve problems deeply. This daily management approach makes OEE goals a part of everyday work.
Case mini‑study: +8–12% OEE in 60 days
This case study shows how a focused approach to improving efficiency can lead to big gains. A team at a custom manufacturing line used a detailed plan to boost output without spending more money.
First, they set a baseline for OEE. They collected data for two weeks and found their score was way off from the industry average. They then made a list of the biggest losses, which showed that Performance Loss was the main issue. Small stops and speed changes were wasting a lot of time.
The team then brainstormed ways to improve the bottleneck equipment. They picked a few key actions to focus on for two weeks. Each task had a specific person and deadline.
The table below shows the plan they followed:
| Countermeasure | Objective | Owner | Timeline | Measured Result |
|---|---|---|---|---|
| 5S Blitz on Constraint | Eliminate tool search time and minor stoppages | Shift Lead | Week 1 | Reduced setup delays by 15% |
| Standardized Fixed Speeds per Product | Eliminate operator speed guesswork and variation | Process Engineer | Week 1 | Reduced speed loss by 22% |
| Visual Andon Alert for Speed Drops | Enable immediate response to line slowdowns | Maintenance Tech | Week 2 | Average response time cut to 2 minutes |
| Detailed Tick Sheet for Small Stops | Capture root causes of frequent, brief stoppages | Line Operator | Week 2 | Identified top 3 recurring issues for future fixes |
They used daily management tools to keep track of progress. A visual alert system was added to the Andon cords, making it easy to see when there were problems.
They measured the results over several production cycles. The changes they made saved a lot of time. This led to an OEE improvement of 8 to 12 percent in just 60 days.
This study shows that following a structured plan can lead to quick improvements. The team was able to increase output without spending more money. This makes it a good example for others to follow.
Template pack: OEE sheet + loss tree
The last step in an OEE improvement plan is to start doing things. Practical tools help make this transition. A template pack gives teams the structure they need to get going.
An OEE calculation sheet helps collect accurate data. It organizes inputs for availability, performance, and quality. This ensures everyone calculates the same way, no matter the shift or line.
A loss tree worksheet sorts out production stops. It matches downtime and defects with the Six Big Losses. This tool makes complex data easy to understand and prioritize.
These templates make the roadmap’s ideas real. They cut down the time it takes to start collecting data. They also give a format for team talks during daily meetings.
These documents speed up the “Information” phase of the IDA cycle. Having consistent data is key for making good decisions. The template pack gives teams the tools to put the plan into action.
Leaders can use these tools to keep focus on important losses. Standard templates turn ideas into real actions. They help teams keep improving OEE over time.


